Every sock goes through the same six stages regardless of who makes it: yarn preparation, knitting, toe closing, boarding and setting, inspection, then packing. The differences between factories are not in the sequence – they are in how tightly each stage is specified and how seriously it is checked.
Knowing the order matters for one practical reason: you can tell which stage a delay is sitting in, and which decisions of yours are causing it. That knowledge is what turns a vague “production is running late” into something you can act on.
The six stages
| Stage | What happens | Your decisions that affect it |
|---|---|---|
| 1. Yarn preparation | Cones inspected, custom shades dyed if required | Colour source – stock card versus dyed to order |
| 2. Knitting | Tube knitted on a circular sock machine | Gauge, construction, pattern complexity |
| 3. Toe closing | Open toe linked or seamlessly joined | Linking versus seamless method |
| 4. Boarding and setting | Heat or steam sets shape | Rarely a buyer choice – often a quality difference |
| 5. Inspection | In-line and final checks against agreed criteria | Sampling standard and pass threshold |
| 6. Packing | Labelled, bagged, cartoned to specification | Barcodes, packaging type, carton marking |
Stage 1: yarn preparation
Cones arrive inspected and, where the programme needs it, are dyed to a confirmed shade. This is the stage that most often adds unexpected calendar days: custom dyeing carries a mill minimum and adds development time before knitting starts.
If your colour can be matched from an existing shade card, that entire step disappears. It is the single easiest schedule saving available and it costs almost nothing in design terms.
Stage 2: knitting
Socks are knitted as tubes on circular sock machines. Coarse gauges suit terry and heavy socks; fine gauges produce a smooth face that takes detail well. Multi-colour pattern work adds yarn changes and more machine minutes per pair, which affects both cost and how much capacity your order consumes.
This is also where complexity becomes schedule risk. A plain style is largely predictable. A complex one may need slower running and closer supervision.
Stage 3: toe closing
The tube leaves the machine with an open toe. Standard linking joins it with a chain stitch – fast and reliable. Seamless or true-linked closing produces a flat, low-bulk join for comfort-led products, and takes longer per pair.
The choice belongs in the first specification rather than discovered during review, because it changes both the quote and per-unit labour time.
Stage 4: boarding and setting
Socks pass over heated forms to stabilise shape. Skipped or rushed setting is a quality failure rather than a cosmetic one: it produces socks that look correct initially but lose shape after washing, which is how returns begin.
Stage 5: inspection
Two checks matter. In-line checks catch problems while knitting is running, before they become a batch. Final checks sample finished pairs against agreed criteria – dimensions, appearance, seam quality.
This stage only works if a standard was agreed first. Ask what gets pulled, what counts as a defect and what the pass threshold is, before production rather than after.
Stage 6: packing
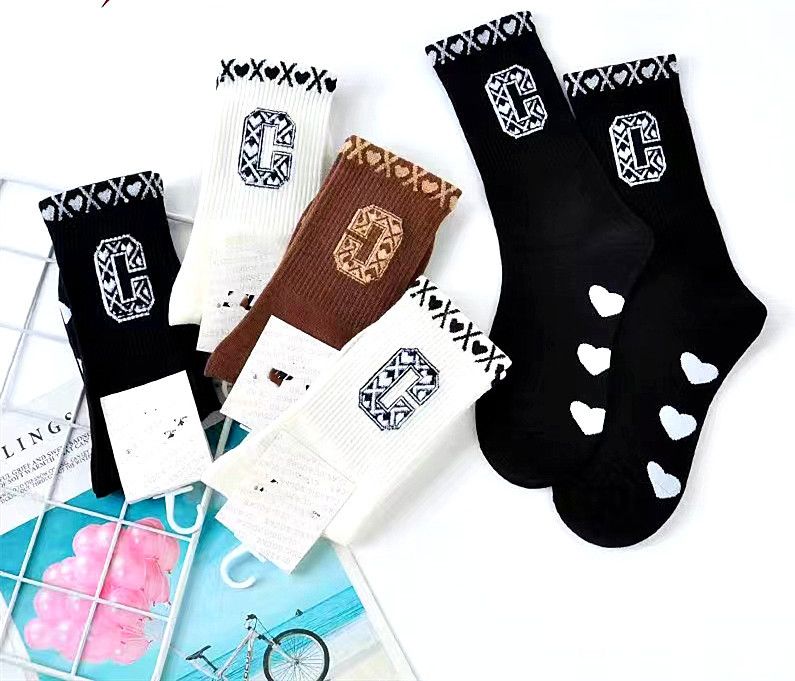
Barcodes, hangtags, belly bands, printed polybags and carton marking all happen here. Most packing errors are specification errors – the factory did what was written, and what was written was incomplete. This is also where your custom sock packaging choices become physical rather than theoretical, and why changes at this stage are disproportionately expensive.
Where schedules actually slip
In our experience four causes account for most delay:
1. Late sample approval. Bulk does not begin until the sample is signed off. This is the most common cause, and the easiest to control.
2. Custom dye lots discovered mid-process. A colour that could have come from a stock card gets specified late as a custom shade.
3. Artwork revised after knitting parameters are set. Changing detail after the gauge is fixed can force restart.
4. Incomplete packing specification. Easy to fix in week one, expensive in week five.
Our reference windows are 3-7 days for sampling and 5-25 days for production after sample approval, with MOQ from 50 pairs per style. The range is wide because gauge, construction and finishing genuinely vary. Ask which part of that window your style falls into, and why.
What to agree before you place an order
Write these down and most disputes never arise:
- Yarn blend and colour source – stock card or dyed to order
- Gauge and complete construction list
- Toe closing method
- Size set and measurements with tolerances
- Inspection standard: sample method, defect list, acceptance threshold
- Packaging and labelling detail, including carton marking
- Artwork locked before production begins
Seasonal programmes such as custom Christmas socks should be planned further ahead than their design suggests – they compete for the same production capacity as everything else.
Ready to move forward? Send a brief through wholesale socks, or begin at Sockmader. Background references are collected on the sock manufacturing process page.
FAQ
How long does production actually take?
Sampling runs 3-7 days, then production takes 5-25 days after sample approval. Where you land in that range depends on gauge, construction and finishing requirements.
Why does my production start date keep moving?
Most commonly because sample approval is still open. Production waits on approval by design – it prevents bulk quantities of an unconfirmed product.
Can I change artwork after knitting has begun?
Technically sometimes, practically at cost. Changes before knitting parameters are locked are cheap; after, they can mean restarting.
What should I ask for on inspection?
A written standard: how many pieces get sampled, what defects are counted, what the acceptance threshold is. Agree it before bulk starts.
Does custom dyeing really add time?
Yes – both development time and, usually, a mill minimum. Taking a near colour from an existing card avoids both.
—
*Parameter note: the figures above are Sockmader’s own production parameters. Confirm any certification or standard referenced against current valid documents before relying on it.*